Compare the three main options
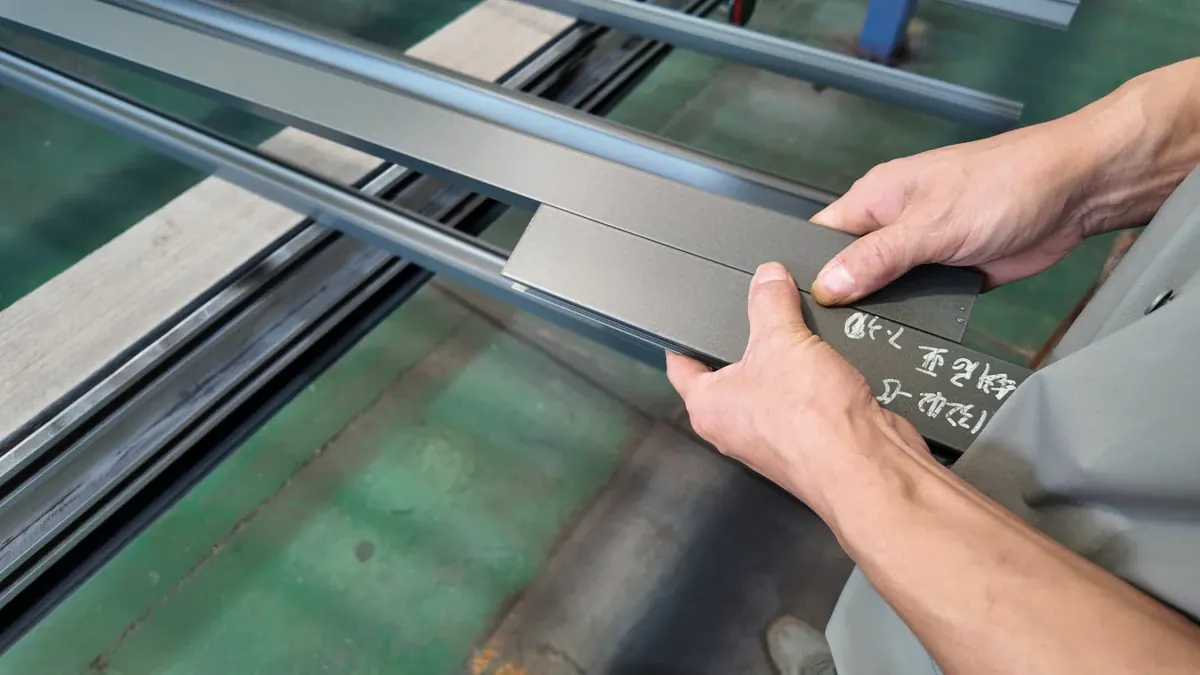
A concealed machine bracket, a visible window frame and a sliding industrial component may need different finishes even when they share the same alloy. Compare the completed part and its exposure rather than choosing from a color chart alone.
| Consideration | Mill finish | Anodizing | Powder coating |
|---|---|---|---|
| Surface | As-extruded aluminum with its naturally formed oxide | An oxide layer formed by an electrochemical conversion process | An applied polymer powder film, thermally cured |
| Appearance | Raw metallic surface; extrusion marks remain visible | Metallic appearance with selected colors and pretreatments | Wide choice of colors, gloss levels and textures |
| Assembly | No additional finishing allowance; extrusion tolerances still apply | Changes precision dimensions; agree pretreatment and oxide-growth allowance | Adds material to surfaces and reduces slot clearance |
| Common uses | Concealed components or parts awaiting further treatment | Decorative and industrial profiles requiring a metallic finish | Architectural and industrial parts requiring an opaque colored finish |
| Cost factors | Usually avoids a separate finishing charge | Film specification, pretreatment, color and batch quantity | Powder system, color changes, geometry, masking and quantity |
| Guantian route | In-house extrusion | Specialist finishing partners | Two in-house powder-coating lines |
When mill finish is appropriate
Mill finish can be practical for hidden components in dry equipment, subframes that will be welded or parts scheduled for another treatment. It avoids a separate decorative finishing stage, but visible die lines, handling marks and variations in the metal remain part of the appearance.
Aluminum does not form red iron rust, yet an unfinished surface can stain or corrode in unsuitable conditions. Outdoor exposure must be assessed for moisture, salt, pollutants, drainage and contact with other materials. For visible architectural work, consider a specified protective finish and an agreed maintenance approach.
When anodizing is worth considering
Anodizing retains a metallic character and can suit selected T-slot frames, electronic housings, decorative trims and industrial components. Film specification and sealing matter to the intended performance. Decorative anodizing should not be treated as interchangeable with a purpose-specified hard-anodizing process for demanding wear applications.
The oxide layer does not conceal deeper machining marks or extrusion weld lines. Alloy, temper, die finish and pretreatment affect the result. Anodizing also changes dimensions: part of the oxide grows into the original surface and part outward, while pretreatment can remove metal. Review precision bores, sliding fits, threads and electrical contact areas with the finishing partner.
When powder coating is the better fit
Powder coating offers a broad range of RAL-based colors, textures and gloss levels for windows, doors, louvers, façades and industrial parts. The powder system and pretreatment must suit the actual exposure. A matte or textured finish may reduce the visibility of minor marks, but coating is not a substitute for an acceptable extrusion surface.
Guantian's documented window project used a powder film of 60–80 µm. The required film and acceptance criteria are confirmed for each order. Review narrow channels, masking and mating parts before die approval. Published cross-cut adhesion targets are grade 0–1, subject to the agreed test procedure and acceptance requirements.
Include wood-grain and electrophoretic finishes in the comparison
Wood-grain transfer uses a powder-coated base and a selected transfer pattern. It can suit decorative windows, doors, furniture and grilles. Approve a representative sample because base color, gloss and profile corners affect the final pattern. Confirm that the selected system is suitable for the intended exposure.
Electrophoretic coating is another option for selected metallic decorative finishes, including champagne or bronze tones. Guantian arranges it through specialist partners. Confirm the available finish, surface preparation, coating specification, minimum quantity and lead time before ordering.
Write the finish into the purchase specification
Identify visible faces, service conditions, color and texture, film requirements, critical finished dimensions and inspection methods. A signed physical sample is more reliable than a color code alone for approving appearance. Agree acceptable variation and any required testing before bulk production.
Published processing lengths are up to 6,500 mm for powder coating and wood-grain transfer, and up to 6,000 mm for partner anodizing and electrophoretic coating. Actual suitability depends on the section and fixturing review.
Frequently asked questions
Is anodizing dimensionally negligible?
No. Its dimensional effect differs from a deposited paint film, but precision features still require an allowance based on pretreatment, alloy and anodizing conditions.
Which finish hides extrusion marks best?
An opaque textured powder coating may make minor marks less noticeable. Clear anodizing generally reveals more of the underlying metal. Confirm appearance on a finished section rather than assuming a finish will conceal defects.
Does a finish determine heat-sink performance?
No. The thermal result depends on the full design and operating conditions. Review contact surfaces and the specified finish with the equipment designer.
Send your installation environment, preferred appearance and critical assembly details. Our team can help compare finishing routes and arrange representative samples.